
By Brad Buecker, SAMCO Technologies
Part 1 of this series1 (a continuation of a POWERGEN 2025 Knowledge Hub presentation) highlighted that even though renewable energy has grown dramatically in recent years, a decades-long need for dispatchable power generation continues, per energy requirements for AI data centers and many other users. Simple- and combined-cycle power plants currently provide much of that power, along with remaining coal and nuclear plants. Nuclear power may enjoy a renaissance, likely in the form of small modular reactors (SMR). Geothermal energy and underground hydrogen deposits have been highlighted in the news recently, and breakthroughs in fusion technology have some utilities looking at real-world applications within a decade or so.2
Most of these technologies require or will require high-purity makeup water. Not to be forgotten are the many steam generators and cogeneration systems at industrial plants such as refineries, steel mills, petrochemical plants and numerous other facilities.
Design prep, know what’s in the raw water
In a previous position, I was part of a team that reviewed the water treatment portion of combined-cycle power plant design specifications. The specs rarely contained anything close to complete raw water analyses and seemed to reflect a much too common mindset, “Water is water, don’t worry about it.” This mistaken belief can cause huge problems with the design and operation of any water treatment system, makeup or otherwise. For example, suspended solids can mechanically foul pretreatment and reverse osmosis (RO) membranes; calcium, magnesium and other cations may combine with bicarbonate, sulfate, silica and other anions to form scale deposits; high chloride concentrations can cause pitting in some metals including the very popular 304 and 316 stainless steels; the list goes on. The table below outlines the major constituents of many freshwater supplies that must be accounted for when designing and operating makeup water treatment systems.

Additional important constituents, although they may exist in slight concentrations, include iron, manganese, barium and strontium. (Many other trace elements/compounds may be critical when evaluating wastewater discharge/treatment issues, but that is a subject for another article.)
Even if design engineers understand the potential impacts of water impurities, they may rely on just a single “snapshot” analysis. However, water chemistry and quality can change both seasonally and due to short-term influences. A classic example of the latter is river water during a heavy rainstorm, where suspended solids concentrations may increase by one or two orders of magnitude very quickly. The large TSS influx can potentially overwhelm pretreatment processes. As a seasonal example, this author directly observed drought conditions one summer that caused the dissolved solids in a lake water supply to increase four-fold between April and August. The TDS increase placed a much greater load on the power plant makeup water system and it induced calcium carbonate scaling in the plant’s once-through steam condensers, where none had occurred before. The proper approach to sampling is to begin raw water testing at project inception and collect data over time that illuminates both seasonal and short-term influences on water chemistry.
Increasingly, plants in freshwater-challenged locations are facing requirements to use alternative supplies. The most common substitute is effluent from a municipal wastewater treatment plant, frequently referred to as a publicly owned treatment works (POTW). Many of these plants have secondary but not tertiary treatment. The table below offers a comparison between four freshwater supplies and the effluent from four POTW plants.

Noticeable in the grey water samples are the much higher concentrations of the major cations (calcium, magnesium, potassium, sodium), anions (chloride, nitrate, phosphate, sulfate), and, of course, conductivity. Ammonia in surface waters is usually inconsequential but for less-than-tertiary-treated grey water is often in double digits (as mg/l), as is evident in the last two samples. Not shown is TOC, which is also typically much higher in wastewater than in fresh water. We will consider POTW pretreatment needs later in this article.
Pretreatment is critical
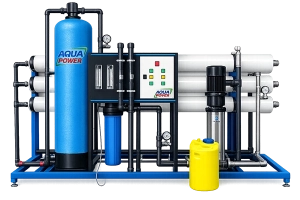
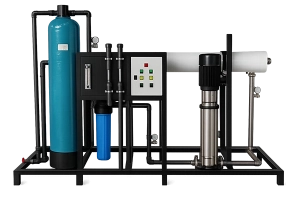
Part 1 highlighted that many modern power plant and cogeneration makeup water treatment systems utilize RO for the core demineralization process. The remainder of this installment and the next article will primarily focus on pretreatment and process treatment methods to protect RO membranes and ensure reliability and smooth operation.
In the power industry, RO really came into vogue in roughly the last three decades of the 20th century as a retrofit ahead of existing ion exchange (IX) demineralizers at coal-fired plants. Figure 1 illustrates the common configuration during this transformation.

Standard for RO units then and now is a set of cartridge filters (5-25 µm, nominal pore size4) immediately upstream of the RO. The cartridge filters capture particulates that escape the pretreatment system, but they do not have the capacity to serve as stand-alone filters.
RO retrofit greatly reduced loading on the IX resins, which in turn lowered the frequency of resin regeneration and improved system reliability. As Figure 1 suggests, primary pretreatment typically consisted of clarification followed by sand or multimedia filtration to remove suspended solids. This author worked with two such systems at a large facility, in which the clarifier/filter effluent turbidity typically ranged between 0.3-1.0 nephelometric turbidity units (NTU). This equated to around three-week intervals between changeouts of the RO cartridge filters. As RO technology matured, other membrane processes emerged, e.g., micro- and ultrafiltration, which have become an increasingly popular substitute for clarification/media filtration for particulate removal. The author served as the lead for a project to replace the first of the two clarifier/filters mentioned above (the second was also subsequently replaced) with a microfilter. Upon MF startup, effluent turbidity levels dropped to a range of 0.027 to 0.036 NTU, where they consistently remained. Cartridge filter replacement frequency decreased from three weeks to three months, another indicator of much improved pretreatment particulate removal. The chart below shows the filtration ranges of the common technologies. A more detailed version of this chart is available in Reference 4.

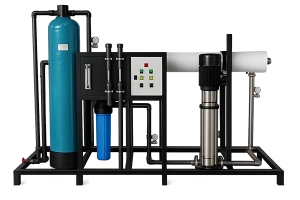
As mentioned in Part 1, many modern HRSG makeup configurations follow the design shown below.

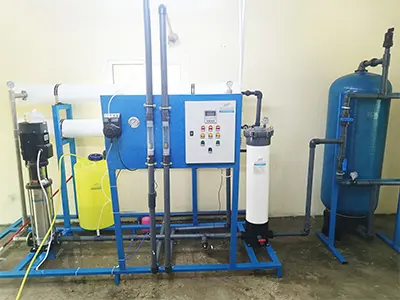
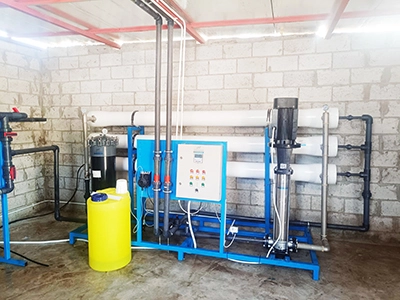
A compact ultrafilter unit is shown in Figure 4.

Cautionary Notes Regarding MF and UF
Cases are known of serious MF and UF fouling by particulates of specific sizes. Per the water testing recommendations mentioned earlier, particulate size analyses should be considered. The data can help a reputable equipment supplier evaluate fouling potential. Furthermore, this author has heard claims from some vendors that MF/UF has no difficulties filtering river water. This view is cloudy (pardon the pun), given that turbidities in some rivers can go sky high during heavy rainfall and potentially blind the membranes.
Another critical RO pretreatment concern is protecting the membranes from attack by oxidizing biocides. We will address this issue in Part 3 of the series, as the most common oxidizer control method is performed just upstream of the RO feed pump.
POTW effluent offers additional challenges
A complete POTW plant has primary, secondary, and tertiary treatment, but many facilities only perform secondary treatment, as that is sufficient to remove pathogenic organisms and allow release of the effluent. However, secondary-treated effluent still contains many impurities in greater concentrations than freshwaters, as was outlined in Figure 1. These include nitrogen species, phosphorus, and organic compounds, all of which can greatly increase the potential for microbiological fouling in makeup, cooling and service water systems.

Clarification/filtration and MF/UF do not remove nitrogen-based impurities, particularly ammonia and nitrite/nitrate. Also, many organics carry through a clarifier. Accordingly, it may be necessary for the industrial plant managers to consider on-site tertiary treatment to remove these impurities. Biological methods to treat both municipal and industrial wastewater have been in place for many years. Well-known is the activated sludge process, in which, following removal of large solids and grit, the waste stream flows into a voluminous basin or basins containing beneficial microorganisms that consume the organics and nitrogen/phosphorus nutrients. The term “activated” comes from the fact that air is injected into the pond, often at numerous locations, to provide an aerobic environment for the microbes. A once-common variation of this technology is that of the trickling filter, in which the wastewater flows over fixed media to which the beneficial organisms are attached. Thus, the microbes have a stable base to carry out waste removal.
A difficulty with either of these technologies is that the treatment processes are slow and require large pond volumes or media surface area. In today’s world of fast start power units that cycle on and off frequently, more robust biological treatment methods are necessary. Two technologies that have emerged as leading candidates are membrane bioreactors (MBR) and moving-bed bioreactors (MBBR). A basic schematic of the former is outlined below.

Having had experience with conventional activated sludge systems, I refer to MBR as “activated sludge on steroids.” The beneficial microorganisms consume the food and nutrients that enter the main vessel from the mixing zone. A recycle stream helps to bring active, well-established organisms to the inlet of the mixing zone. A major difference of MBR from conventional technology is the use of microfilter membranes rather than a clarifier to separate solids from the effluent. The microfiltration process produces a very clear stream, essentially free of suspended solids. One deficiency of this basic design is that ammonia in the stream is converted to nitrite/nitrate, but the nitrogen remains. Nitrites and nitrates can still serve as a nutrient in industrial plant water systems. This problem can be solved, if necessary, by expanding the MBR configuration to include anoxic or anaerobic reaction chambers that have microorganisms to convert nitrite/nitrate to elemental nitrogen.6
Regarding MBBR, the main reaction vessel includes mobile plastic media that serves as sites for the beneficial microorganisms to attach and then consume nitrogen species, phosphorus, and organic compounds. MBBR can be thought of as an advanced version of the trickling bed wastewater treatment process, with the beneficial microbes attached to mobile rather than fixed media. Due to the use of these media in the reaction vessel, filtration membranes cannot be placed in this compartment. Rather, filtration must be separately performed on the system effluent.
Conclusion
This series, with Part 3 coming out soon, serves as a follow-up to a well-received POWERGEN 2025 “Knowledge Hub” presentation. POWERGEN 2026 (January 20-22, 2026, San Antonio, Texas) promises to expand the discussion of steam generation, cooling water and makeup water treatment technologies, especially because the annual Electric Utility & Cogeneration Chemistry Workshop (EUC2W) will now be co-locating with POWERGEN. Watch for further announcements.
Disclaimer
This article offers general information and should not serve as a design specification. Every project has unique aspects that must be individually evaluated by experts from reputable water treatment and engineering firms. Also, any issues that could potentially have an environmental influence, for example, wastewater discharge from a proposed makeup, process, or cooling water treatment system, must be presented to and approved by the proper environmental regulators during the project design phase.
References
- POWERGEN highlights the importance of water and steam chemistry
- Type One Energy and TVA enter agreement to advance fusion deployment
- Post, R., and Buecker, B., “Grey Water – A Sustainable Alternative for Cooling Water Makeup”; Paper 18-17 from the 2018 International Water Conference, November 2018, Scottsdale, Arizona.
- W. Byrne, Reverse Osmosis: A Practical Guide for Industrial Users, Tall Oaks Publishing, Littleton, Colorado, 2002.
- Post, R., Buecker, B., and Shulder, S., “Power Plant Cooling Water Fundamentals”; pre-workshop seminar for the 37th Annual Electric Utility Chemistry Workshop, June 6-8, 2017, Champaign, Illinois.
- https://samcotech.com/technologies-innovations/biological/membrane-bioreactor-mbr/
About the Author: Brad Buecker currently serves as Senior Technical Consultant with SAMCO Technologies. He is also the owner of Buecker & Associates, LLC, which provides independent technical writing/marketing services. Buecker has many years of experience in or supporting the power industry, much of it in steam generation chemistry, water treatment, air quality control, and results engineering positions with City Water, Light & Power (Springfield, Illinois) and Kansas City Power & Light Company’s (now Evergy) La Cygne, Kansas, station. Additionally, his background includes eleven years with two engineering firms, Burns & McDonnell and Kiewit, and he spent two years as acting water/wastewater supervisor at a chemical plant. Buecker has a B.S. in chemistry from Iowa State University with additional course work in fluid mechanics, energy and materials balances, and advanced inorganic chemistry. He has authored or co-authored over 300 articles for various technical trade magazines, and he has written three books on power plant chemistry and air pollution control. He is a member of the ACS, AIChE, AIST, ASME, AWT, CTI, and he is active with Power-Gen International, the Electric Utility & Cogeneration Chemistry Workshop, and the International Water Conference. He can be reached at [email protected] and [email protected].